 fuyuhuaxue@iumrs.com
Ask a plant engineer what keeps them up at night, and you’ll hear the usual suspects: equipment downtime, supply chain delays, safety incidents, labor shortages. Nobody says “the floor.” And yet, when a floor fails, it touches all of those things at once. A delaminating coating becomes a trip hazard and a safety report. A dusting slab contaminates product and triggers quality holds. A cracked, porous surface traps oil and wash water, turning cleaning into a daily battle and slowing every changeover.
The floor is the platform everything else runs on. When it works, nobody notices. When it doesn’t, everyone does.
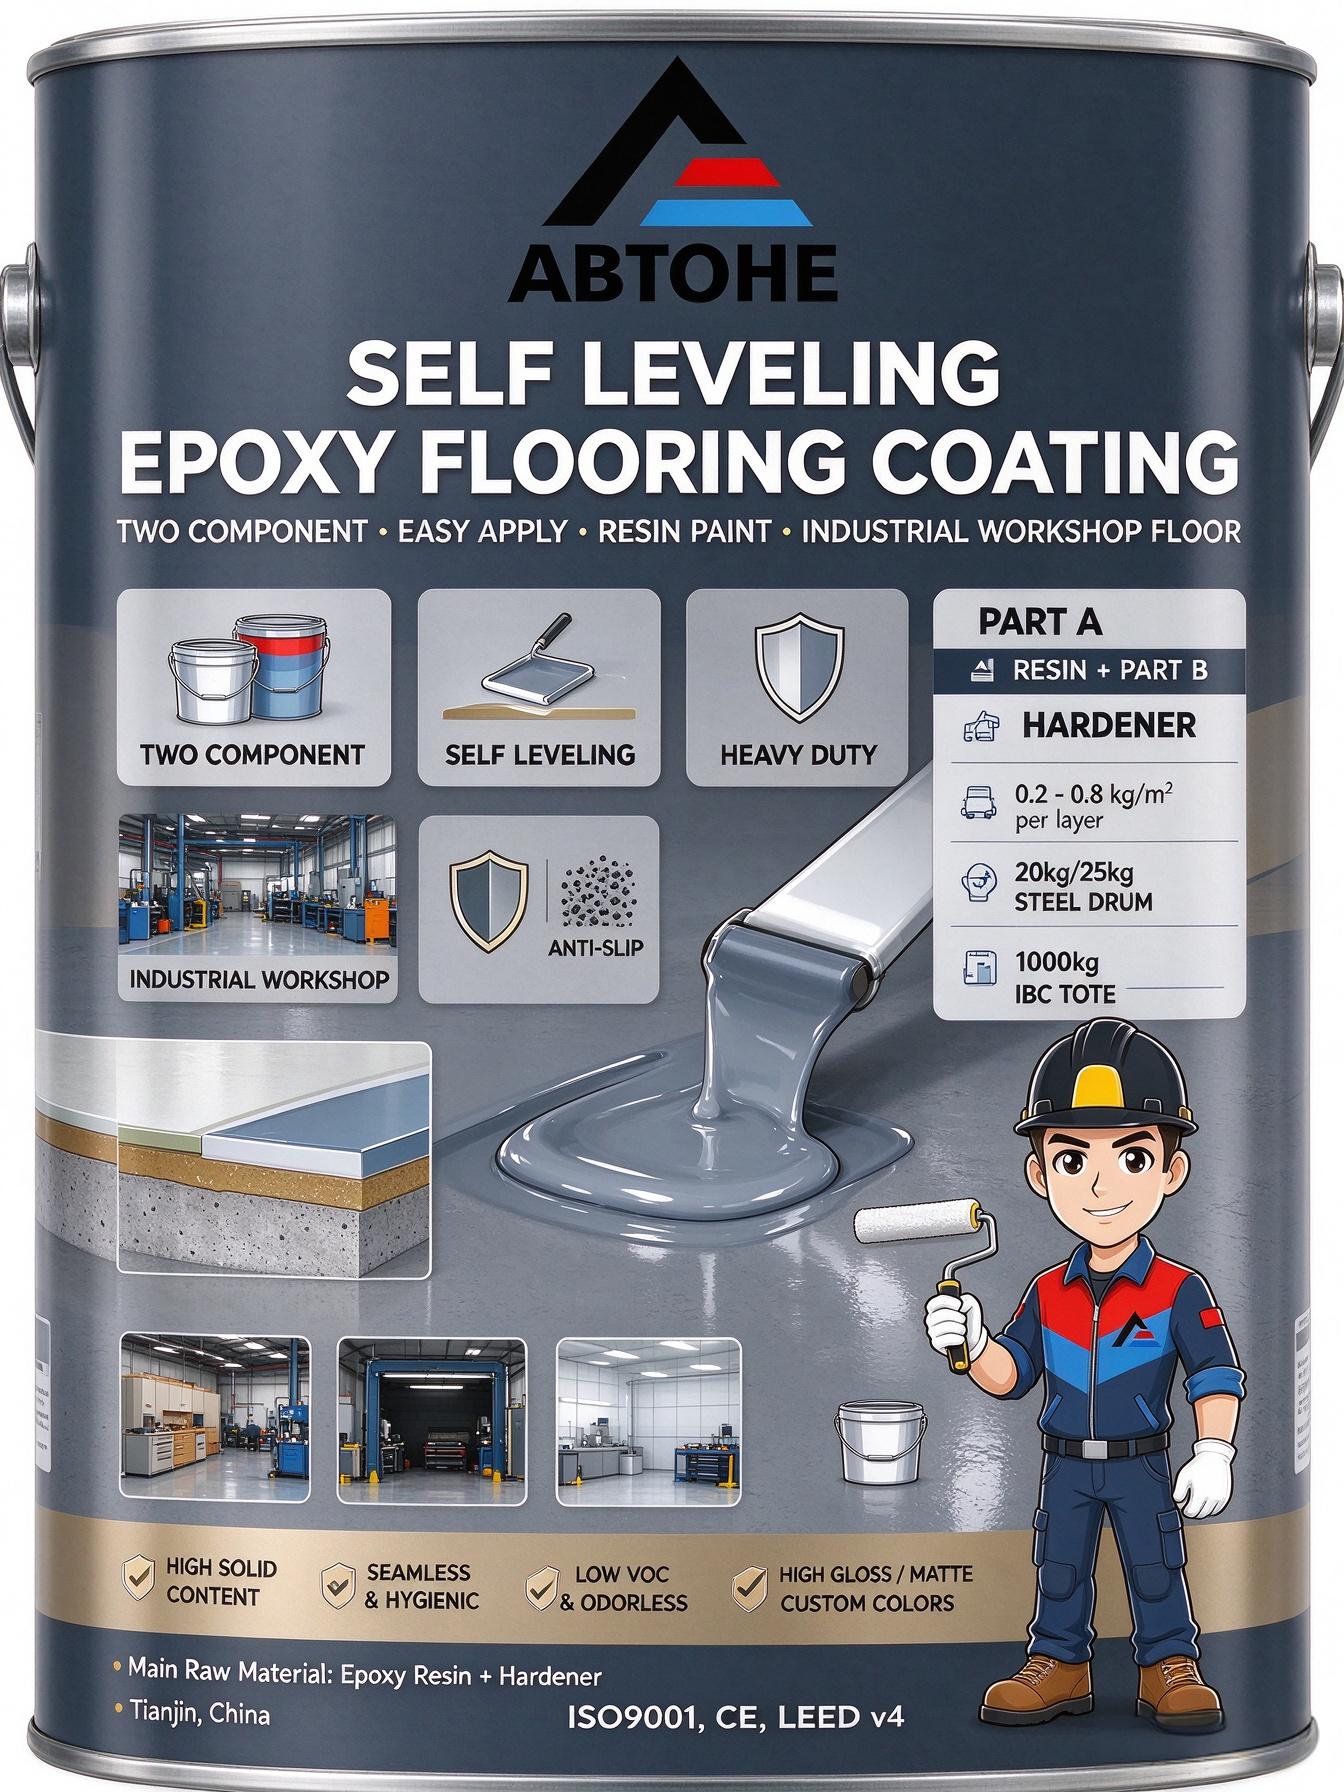
The ABTOHE Self-Leveling Epoxy Flooring Coating was engineered for exactly this reality. It’s a two-component epoxy system—Part A resin and Part B hardener—designed for industrial workshop floors, warehouses, garages, and cleanrooms. It’s supplied from Tianjin, China, ISO 9001 and CE certified, LEED v4 compliant, and available in 20kg/25kg steel drums or 1000kg IBC totes for bulk buyers, with full OEM/ODM support for private labeling and custom formulations.
It’s not a product that asks for attention. It’s a product that earns trust by disappearing into the background and staying there.
Let’s walk through why that matters.
The Epoxy Resin Base: Where the Performance Comes From
Every epoxy floor coating makes a promise. The difference is whether the chemistry behind that promise can deliver over years of industrial abuse.
This system is built on an epoxy resin base with a two-component resin and high-efficiency hardener system. That chemistry produces a strong adhesion matrix—formulated for superior cross-linking bonding with concrete substrates—so the coating doesn’t just sit on the slab. It bonds to it.
That bonding matters more than most buyers realize. Adhesion is what prevents peeling or lifting under heavy traffic—the failure mode that turns a floor investment into a liability. When a coating lifts, it becomes a trip hazard, a moisture trap, and a repair project. When it stays bonded, it protects the substrate for the full service life of the floor.
The epoxy base also delivers chemical resistance and heavy-duty wear resistance, which makes the system suitable for a broad range of industrial and individual applications—from workshops handling oils and solvents to garages, warehouses, and cleanrooms where cleanliness and durability are non-negotiable.
Dust-Proof and Anti-Slip: Two Problems, One Solution
Bare concrete dusts. It’s not a cosmetic issue. Dust contaminates products, clogs machinery, coats surfaces, and creates respiratory hazards. It also means the slab is slowly eroding, generating new dust every day.
This coating is dust-proof, sealing the concrete surface and locking particles in place. The floor stops shedding. Cleaning becomes maintenance rather than a losing battle, and the air in the facility gets measurably cleaner.
At the same time, the system is anti-slip, which enhances the safety and cleanliness of the floor and reduces the risk of accidents and maintenance needs. In industrial environments where oil, water, and cleaning chemicals are part of daily operations, slip resistance isn’t a nice-to-have—it’s a core safety requirement. The coating’s slip-resistant textures can be customized with quartz or flake aggregation to match the specific demands of the space, so you get grip where you need it without sacrificing the finish.
Dust-proof and anti-slip together solve the two most persistent complaints about industrial floors in a single system.
High Solid Content: Leveling, Thickness, and Forgiveness
Here’s where the product separates itself from thin-film floor paints.
High solid content means more of what you apply stays on the floor as a protective film, rather than evaporating away as solvent. In practice, that delivers excellent leveling properties and thick-film build—a coating that flows out smoothly and builds substantial film thickness in fewer coats.
That thick-film build does two useful things. First, it easily hides minor concrete imperfections, which means a less-than-perfect slab doesn’t require extensive patching and leveling before coating. Second, it delivers more protection per layer, which translates into better wear resistance and longer service life.
For contractors, high solid content means fewer coats, faster completion, and a more forgiving substrate. For facility owners, it means a floor that looks finished and behaves durably, even when the slab underneath was less than ideal.
Seamless and Hygienic: No Cracks, No Joints, No Hiding Places
Cracks, joints, and seams are where industrial floors go wrong. They trap dirt, moisture, oil, and bacteria. They’re impossible to clean properly and impossible to keep sanitary. In food-adjacent facilities, cleanrooms, and pharmaceutical environments, they’re a compliance problem. Everywhere else, they’re a maintenance burden.
This coating cures into a seamless, hygienic surface that eliminates cracks, joints, and seams where dirt, moisture, and bacteria can accumulate. The floor becomes a single continuous plane—easy to mop, easy to sanitize, easy to inspect.
That seamless quality is especially valuable in cleanrooms, where surface integrity is part of the contamination-control strategy, and in facilities pursuing GMP or similar standards where cleanability is audited rather than assumed.
It’s also simply better for daily operations. A seamless floor takes less time to clean, requires fewer chemicals, and stays presentable longer. Over a year, that adds up to real labor savings.
Strong Adhesion Matrix: Built to Stay Put
We touched on adhesion earlier, but it deserves a closer look because it’s the foundation of everything else.
The system is formulated for superior cross-linking bonding with concrete substrates, which is the technical way of saying it grips the slab at a chemical level rather than simply sticking to the surface. That bond is what prevents peeling or lifting under heavy traffic—forklifts, pallet trucks, carts, and constant footfall all test adhesion continuously, and a coating that isn’t properly bonded will fail at the edges first, then spread inward.
Strong adhesion also matters when the slab moves. Concrete expands and contracts with temperature, and a coating that can’t move with it will crack or delaminate. A properly cross-linked system accommodates that movement while staying bonded, which is why the floor performs through seasonal cycles rather than failing in the first temperature swing.
For project buyers, adhesion is the specification that determines whether the floor lasts five years or fifteen.
Low VOC and Odorless Options: Greener Chemistry, Safer Application
Industrial coatings have historically been unpleasant to apply—strong fumes, heavy ventilation requirements, and lingering odor that makes occupied spaces unusable for days.
This system offers low VOC and odorless options, with an environmentally friendly formulation compliant with international green building standards. That compliance isn’t just paperwork. It matters for:
- Indoor air quality in facilities where people work every day
- Application safety for the crews installing the floor
- Occupied-space projects where operations can’t fully pause
- Green building certification for projects pursuing LEED or similar standards
- Corporate sustainability targets that increasingly include building materials
The product is LEED v4 compliant, which is a meaningful credential for project buyers working on certified buildings or sustainability-driven specifications. It also aligns with the broader shift in the coatings industry toward lower-emission chemistry—a shift that’s driven by regulation, yes, but also by customer expectation.
For contractors, low-VOC formulations open up scheduling options and make sensitive-environment work feasible. For facility managers, they mean a floor that can be installed without disrupting the people who use the building.
High Gloss, Matte, Clear Topcoat, and Anti-Slip Finishes
The product is available in a range of finishes: high gloss, matte, clear topcoat, and anti-slip. That flexibility matters because different spaces have different requirements.
High gloss reflects light, brightens the space, and makes cleaning easy—ideal for showrooms, cleanrooms, and areas where appearance signals quality.
Matte reduces glare and provides a more understated, industrial look—useful in large production halls where reflective surfaces can cause eye strain.
Clear topcoat protects decorative finishes or colored substrates while letting the underlying surface show through.
Anti-slip adds texture for traction in wet or oily areas, available with quartz or flake aggregation to match the environment’s demands.
Colors are customizable based on RAL and Pantone color charts, which means the floor can be matched to brand standards, safety color codes, or project design requirements. For facilities using color-coded zoning—walkways, storage, hazard areas—that customization is a functional tool, not just an aesthetic option.
Coverage Rate and Application
Practical projects need practical numbers. Coverage is 0.2–0.8 kg per square meter per layer, depending on film thickness and substrate condition. That range gives contractors and estimators the flexibility to plan material quantities accurately across different project types.
Application is flexible: brush, roller, squeegee, or trowel. That means the same product can be applied by different crews with different equipment and still deliver consistent results. For smaller areas or detail work, brush and roller are sufficient. For large floors, squeegee or trowel application speeds things up and helps achieve the thick-film build the system is designed for.
The two-component format—Part A resin plus Part B hardener—is standard, straightforward, and familiar to anyone with epoxy experience. Mixing is simple, and the self-leveling behavior helps the coating settle into a smooth, uniform finish.
Packaging and Bulk Supply
Industrial buyers need industrial packaging. The product ships in 20kg/25kg steel drums for standard orders, or 1000kg IBC totes for bulk projects and distributor stocking. That range covers everything from a single workshop floor to a multi-site rollout.
Certifications include ISO 9001, CE, and LEED v4 compliance, with product testing documentation available—the kind of credentials that procurement teams and project specifiers need to clear internal approvals.
The manufacturer supports full OEM/ODM service, including customized formulas and private labeling. For distributors and importers, that’s the opportunity to build a proprietary product line rather than competing on commodity pricing. For project buyers, it’s the ability to specify a coating tailored to the exact demands of the site.
Where This Floor Belongs
The application range reflects the product’s industrial focus:
- Warehouses – heavy-duty wear resistance under pallet trucks and storage
- Industrial workshops – chemical resistance, dust-proofing, and impact resistance
- Garages – oil, fuel, and tire mark resistance with easy cleaning
- Cleanrooms – seamless, hygienic, and low-VOC options for sensitive environments
- Production halls – seamless surfaces that support 5S and cleanliness standards
- Commercial and industrial facilities – durable, customizable, and certified
It’s also suitable for road marking paint applications, given its durability and color customization, which extends its usefulness beyond interior floors.
The Technical Snapshot
- Brand: ABTOHE
- Product: Self-Leveling Epoxy Flooring Coating, Two Component
- Place of Origin: Tianjin, China
- Main Raw Material: 2-component epoxy resin and high-efficiency hardener system
- State: Liquid coating (Part A resin + Part B hardener)
- Classification: Chemical auxiliary agent / polymer surface coating
- Usage: Building coating, road marking paint; warehouses, industrial workshops, garages, cleanrooms
- Application Method: Brush, roller, squeegee, or trowel
- Finish: High gloss, matte, clear topcoat, anti-slip
- Color: Custom colors based on RAL and Pantone color charts
- Coverage Rate: 0.2–0.8 kg per square meter per layer
- Features: Heavy-duty wear resistant, dustproof, chemical proof
- Certification: ISO 9001, CE certified, LEED v4 compliant, product tested
- OEM/ODM: Fully supported—customized formulas and private labeling
- Packaging: 20kg/25kg steel drum or 1000kg IBC tote for bulk orders
- Single Package Size: 32 × 32 × 40 cm
- Single Gross Weight: 20.0 kg
Key highlights:
- High solid content for excellent leveling and thick-film build that hides minor imperfections
- Seamless, hygienic surface with no cracks, joints, or seams for dirt and bacteria
- Strong adhesion matrix for superior cross-linking bonding and resistance to peeling under traffic
- Low VOC and odorless options compliant with international green building standards
- High gloss and matte finishes in standard RAL colors, with customizable slip-resistant textures
Who This Product Is For
Plant managers and facility engineers who are tired of dust, failed coatings, and repeated repairs—and want a floor that stops generating work orders.
Contractors who need a high-solid, self-leveling system that applies with standard tools and delivers a consistent, professional finish.
Distributors and importers looking for an ISO-certified, CE-marked, LEED-compliant product with OEM/ODM support and bulk packaging options.
Project buyers and specifiers who need documentation, certifications, and a manufacturer that can support large-scale procurement.
Cleanroom and hygiene-sensitive operators who need a seamless, low-VOC surface that supports contamination control.
The Bottom Line
Industrial floors are judged by what they don’t do. They don’t dust. They don’t crack. They don’t peel. They don’t collect dirt in joints. They don’t fail under traffic. They don’t create safety incidents or quality holds or maintenance backlogs.
The ABTOHE Self-Leveling Epoxy Flooring Coating is built to meet that standard. It combines an epoxy resin base and high-efficiency hardener for strong adhesion and chemical resistance, high solid content for leveling and thick-film build, dust-proof and anti-slip performance for safety and cleanliness, a seamless hygienic surface with no cracks or seams, low VOC and odorless options for greener application, and customizable finishes and RAL colors to match any environment.
It’s ISO 9001 and CE certified, LEED v4 compliant, available in bulk packaging, and fully supported for OEM/ODM customization.
If your workshop floor is still bare concrete—dusting, staining, and waiting for its first failure—this is the upgrade that pays for itself quietly, every shift, for years.
ABTOHE Self-Leveling Epoxy Flooring Coating. Seamless. Wear-resistant. Dust-proof. Built for the floor under the work.