 fuyuhuaxue@iumrs.com
Warehouse floors are judged by a brutal standard. No one praises them. No one photographs them. They simply have to survive—through forklifts, pallet trucks, dropped loads, chemical spills, constant footfall, and years of cleaning—without cracking, peeling, dusting, or becoming a safety hazard. The moment a warehouse floor fails, it becomes the most expensive square meter in the building.
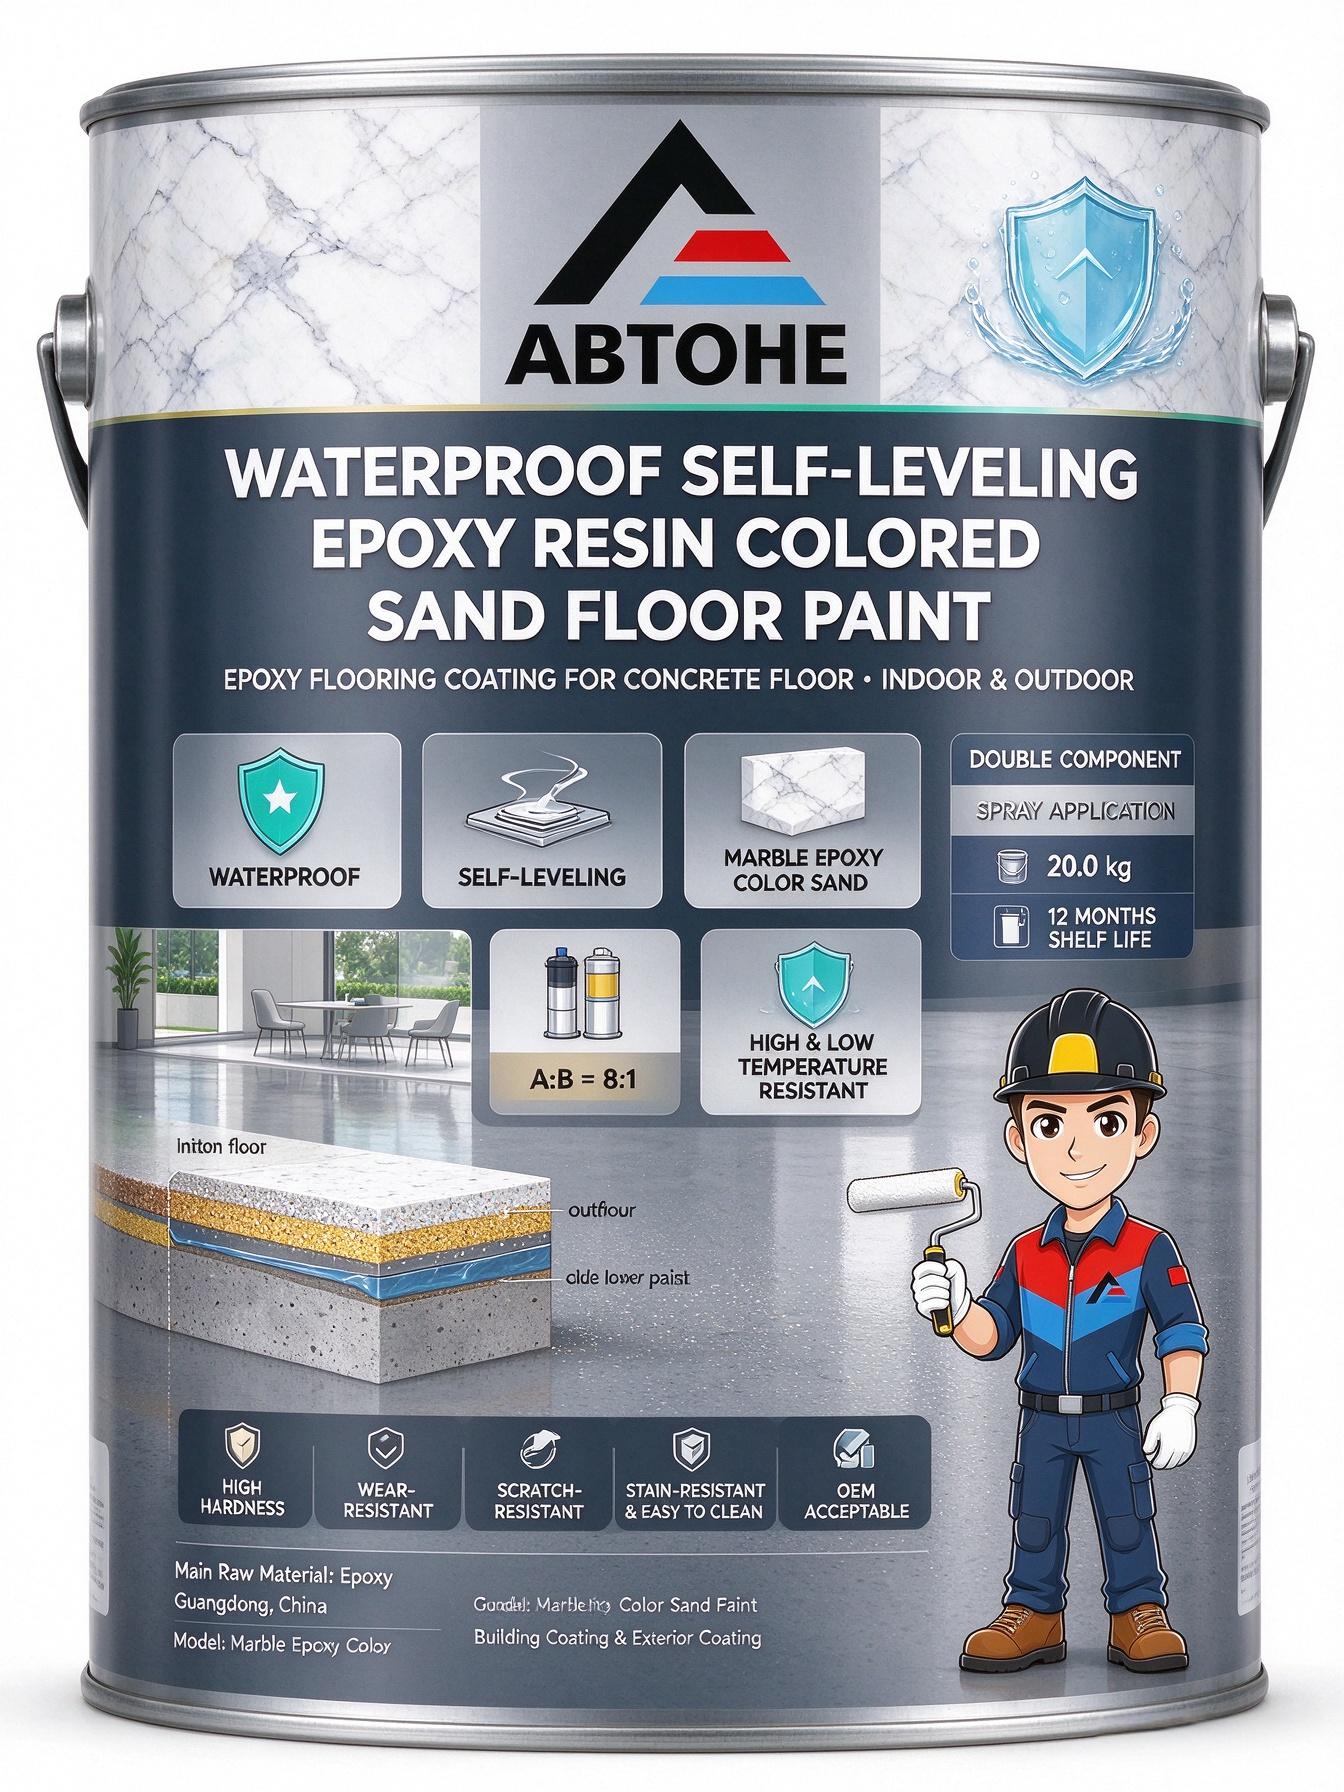
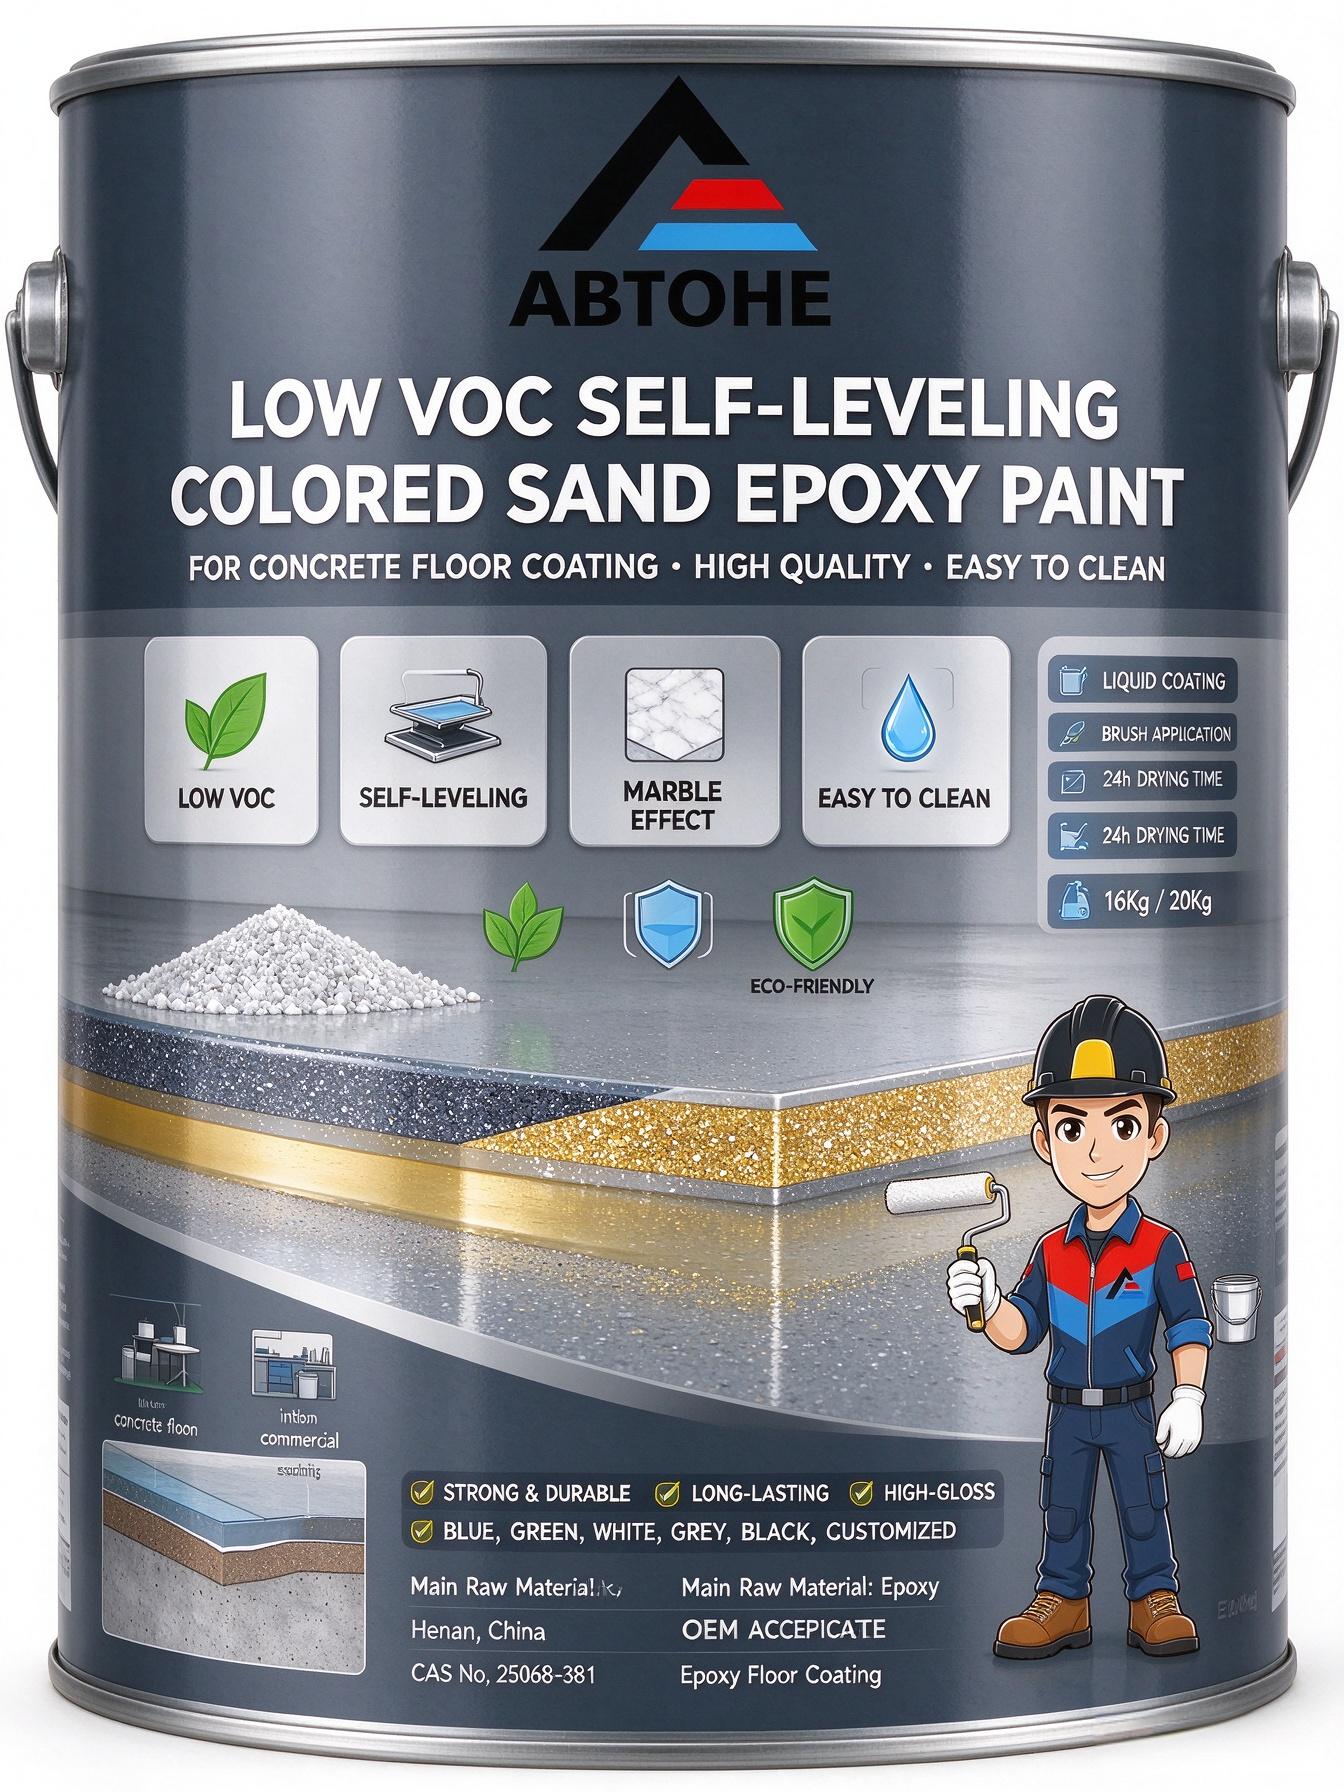
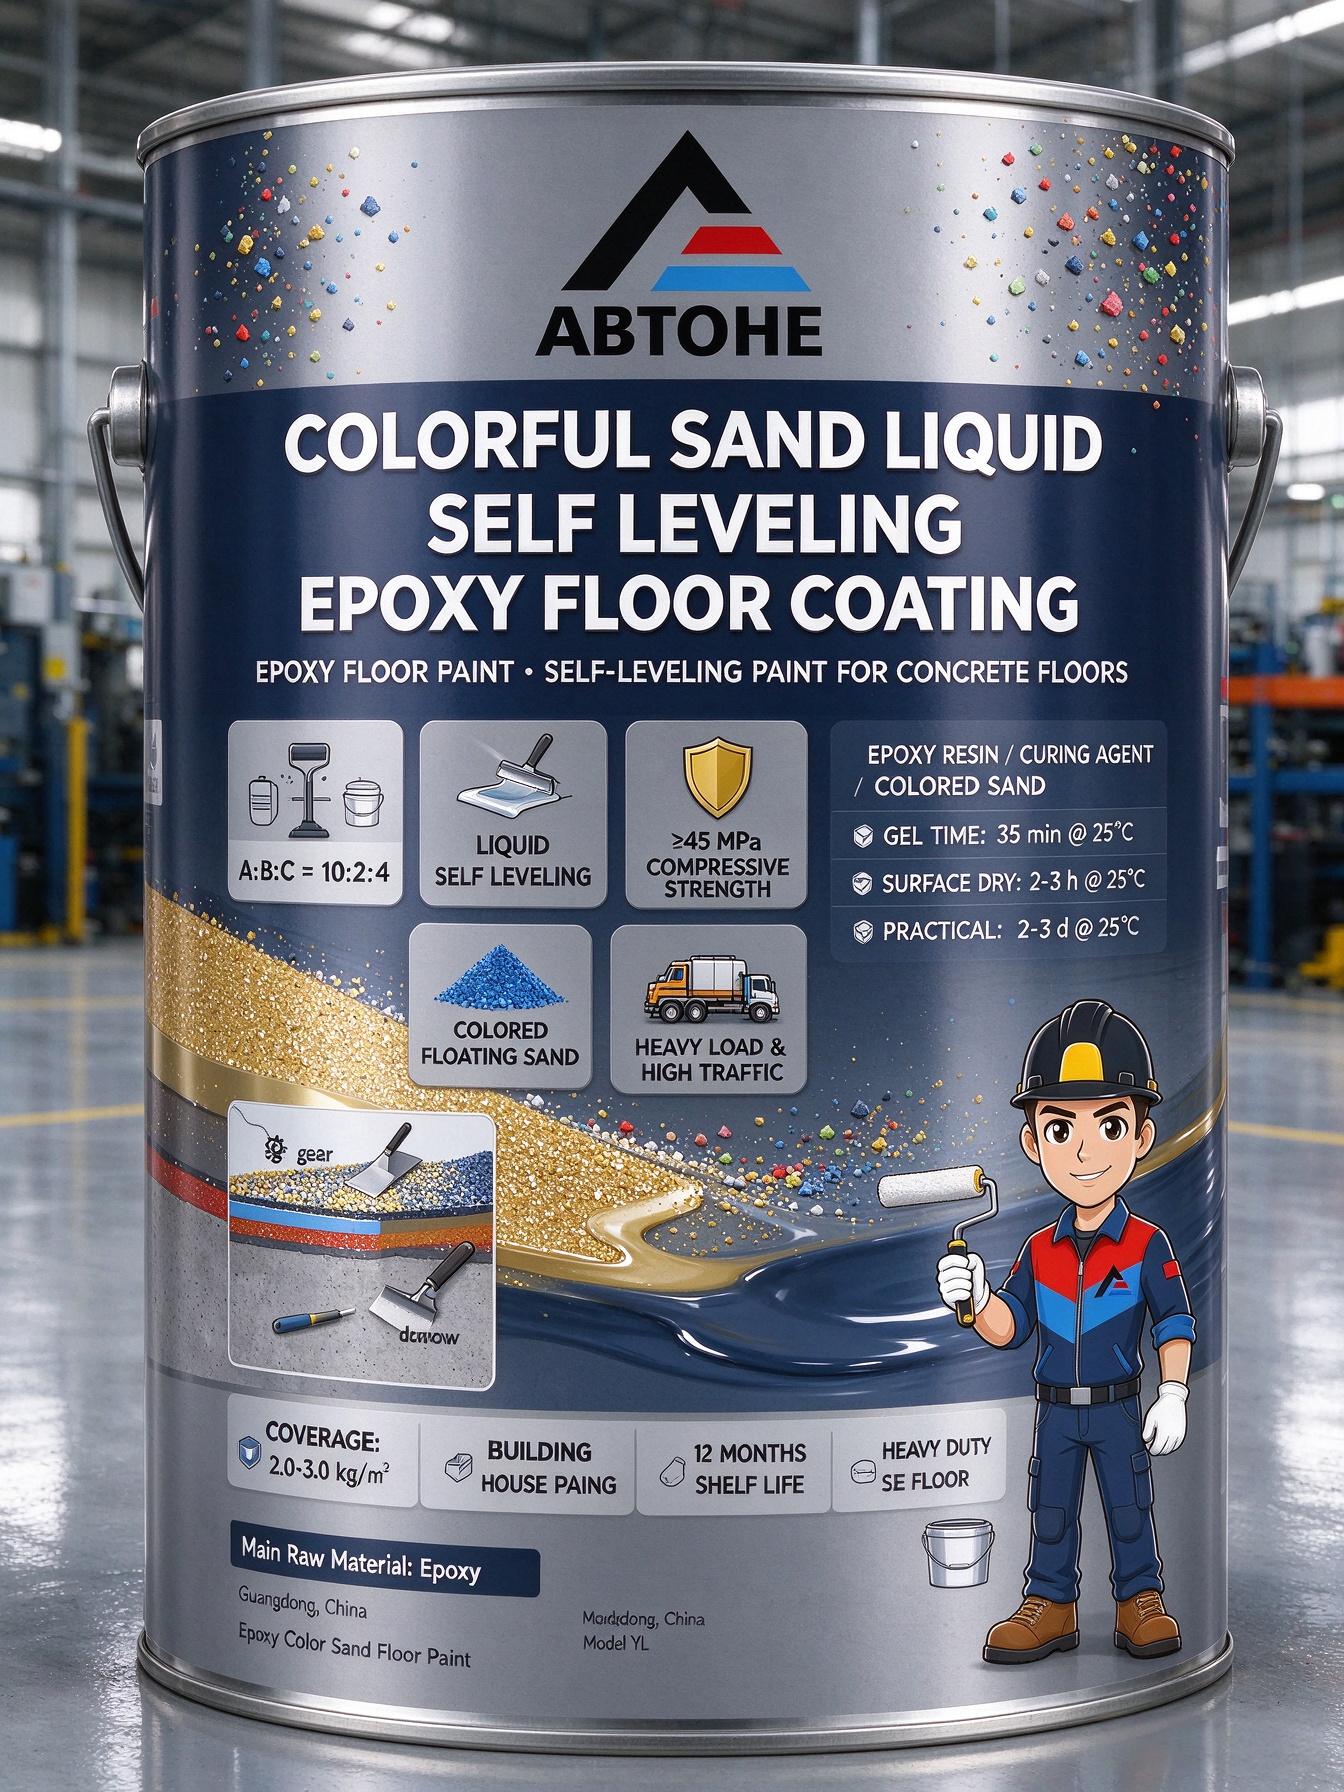
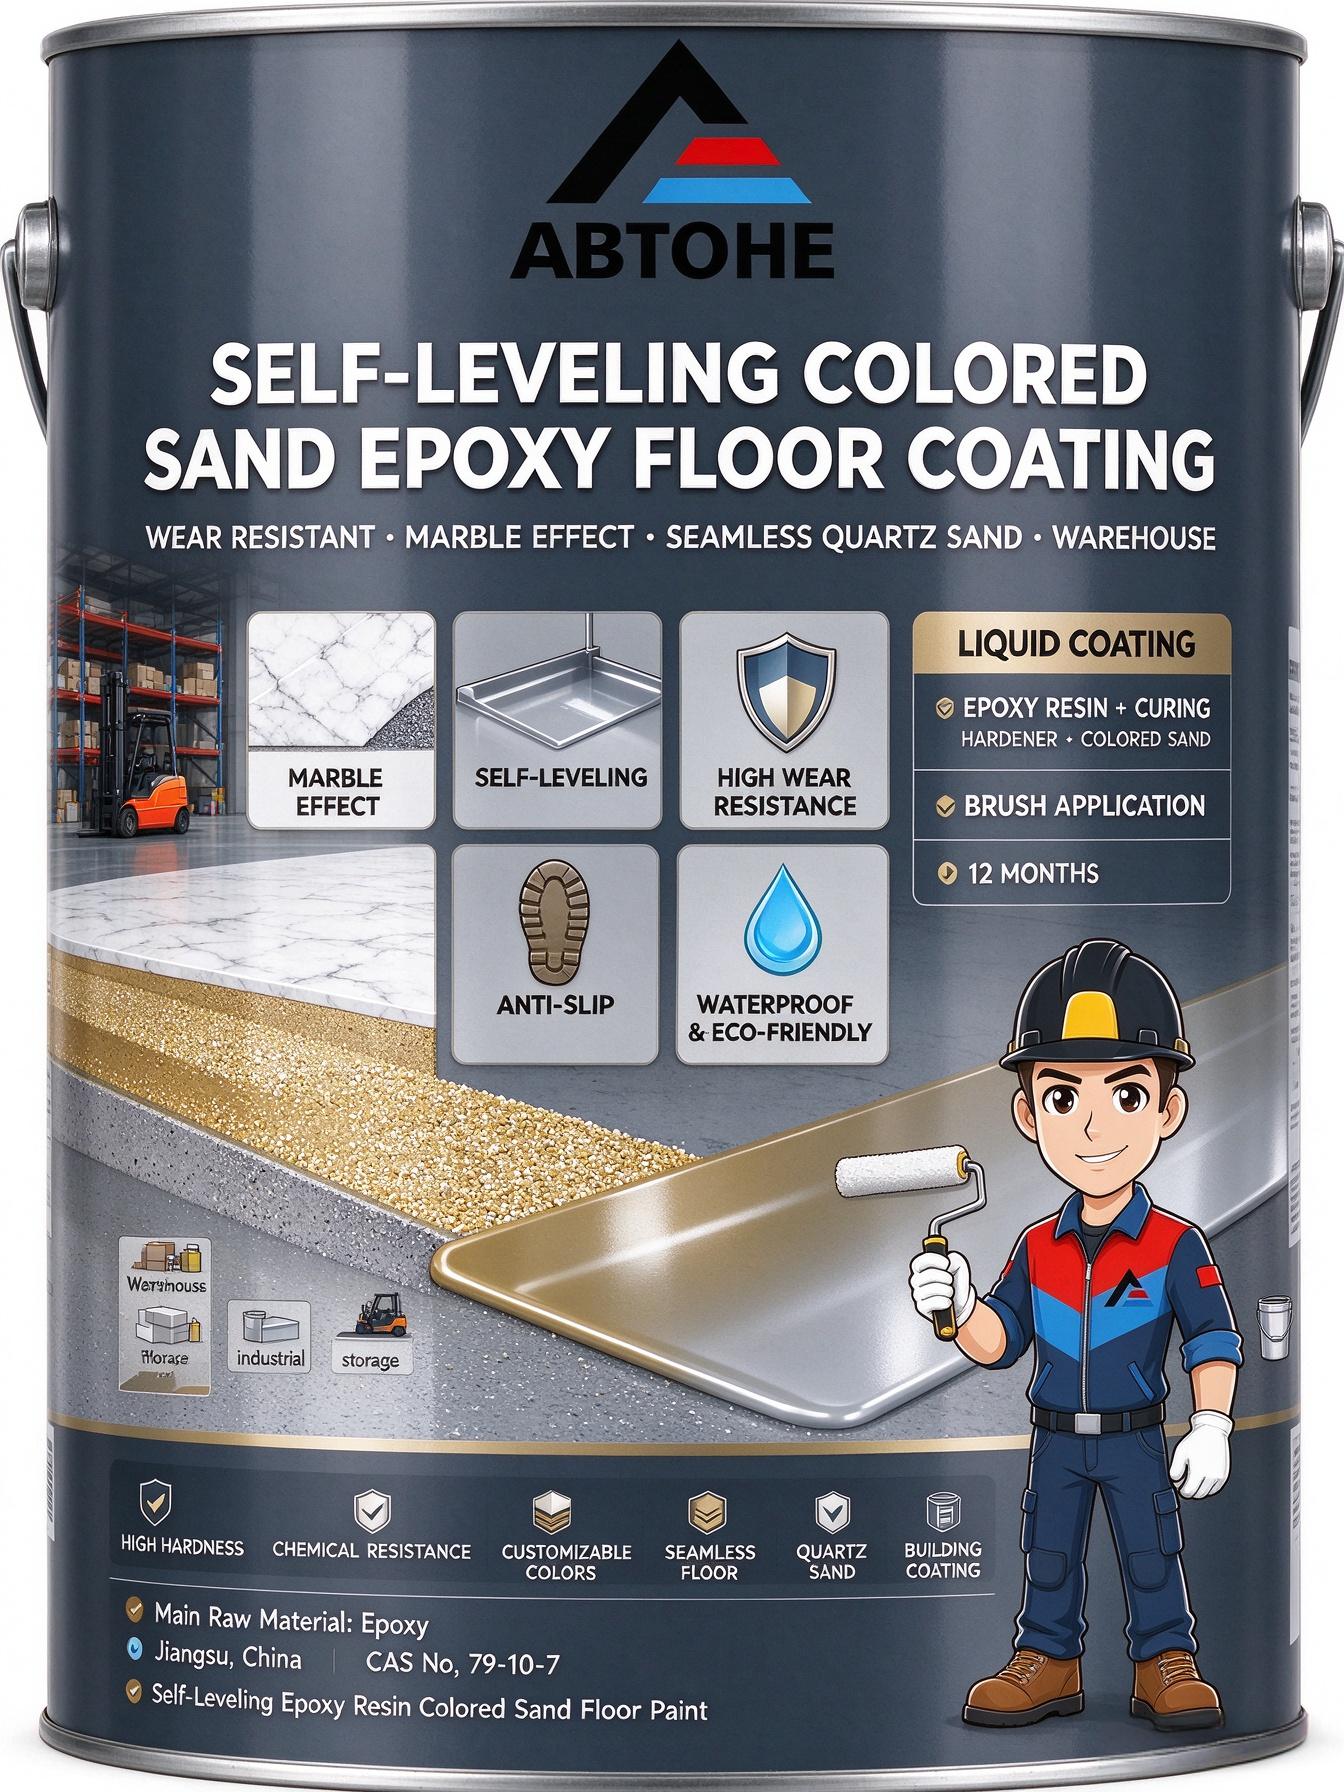
That’s the reality the ABTOHE Self-Leveling Colored Sand Epoxy Floor Coating was designed for. It’s a liquid epoxy system combining epoxy resin, curing hardener, and colored sand to create a wear-resistant, marble-effect, seamless quartz sand floor built specifically for the demands of warehouses and other high-traffic industrial environments.
Manufactured in Jiangsu, China, certified with a 12-month shelf life, and available in rich, customizable colors, it’s a product that refuses to accept the trade-off between toughness and appearance. It delivers both—and it does so with an application process simple enough to use a brush.
Let’s break down why this floor belongs in your warehouse.
Self-Leveling: Even Results Without the Skill Barrier
The first thing that separates this product from ordinary floor paints is its self-leveling behavior.
After application, the coating ensures even application without manual leveling—it flows out and settles into a flat, uniform film on its own. That means the applicator doesn’t need to achieve perfect results through technique alone. The chemistry does the heavy lifting.
For a warehouse, that matters in two ways. First, it means a faster installation—crews spend less time fighting the material and more time moving through the project. Second, it means a more consistent finish—uniform thickness, uniform performance, and no high or low spots that become wear points or puddles.
The application method is listed as brush, which makes the system accessible for touch-ups, edges, and smaller areas, while larger floors can be handled with a roller or squeegee to spread the material before it self-levels. The result is a seamless surface with no joints, grout lines, or overlaps—one continuous floor that performs as a single system.
Seamlessness isn’t a cosmetic detail in a warehouse. Joints are where dirt collects, where moisture penetrates, and where coatings begin to fail. A seamless floor eliminates those vulnerabilities and makes cleaning dramatically easier.
High Wear Resistance: Built for Forklift Traffic
Warehouse floors take abuse that residential and light commercial floors never see. Forklift wheels, pallet trucks, steel-toed boots, dragged equipment, and the constant grind of grit underfoot all test the coating’s durability every single day.
This product delivers high wear resistance, resisting scratches and abrasion for durability. The epoxy resin forms a hard, dense film, and the colored sand aggregate reinforces that film—distributing stress, resisting gouges, and maintaining surface integrity under traffic.
For warehouse operators, that means:
- No powdering that contaminates stored goods
- No peeling that creates trip hazards
- No rapid wear-through in traffic lanes
- No delamination under rolling loads
The floor stays functional, which is the single most important thing a warehouse floor can do. Every square meter that stays intact is a square meter that isn’t generating a maintenance ticket, a safety report, or a repair project.
Chemical Resistance: Safe for Demanding Industrial Environments
Warehouses store and move everything—oils, solvents, cleaning chemicals, fuels, and a wide range of industrial substances. Spills are not a possibility; they’re an inevitability.
This coating is resistant to harsh chemicals, making it safe for use in demanding industrial environments. Spills sit on the surface rather than soaking in, and they can be wiped up before they cause damage. The coating doesn’t soften, blister, or discolor when exposed to the substances it’s likely to encounter.
That chemical resistance also protects the substrate beneath. A floor that resists chemicals keeps the concrete sealed and protected, which extends the life of the slab and avoids the costly cycle of repair and replacement.
For warehouse managers, that means fewer chemical-related floor failures and a more resilient facility overall.
Anti-Slip Surface: Safety Underfoot
Slips and falls are among the most common workplace accidents, and warehouse floors—with their mix of smooth surfaces, rolling equipment, and occasional spills—are a high-risk environment.
This product provides an anti-slip surface that delivers excellent traction to prevent accidents. The colored sand structure creates a natural micro-texture that grips underfoot, and because that texture is part of the coating rather than a surface treatment, it doesn’t wear away over time.
That’s a critical distinction. Many anti-slip floors rely on added grit or temporary treatments that degrade with traffic. This system builds traction into the floor itself, which means the safety performance persists for the life of the coating.
For a warehouse, that’s a compliance-friendly surface and a genuine safety improvement. For the people working on the floor every day, it’s the difference between confidence and caution.
Eco-Friendly, Waterproof, and High Hardness
The product carries a combination of features that make it practical for modern warehouses:
Eco-friendly. The formulation is designed to reduce environmental impact—important for facilities pursuing sustainability targets and for the people applying and working around the product.
Waterproof. The coating seals the surface against moisture, protecting the concrete beneath and making the floor easy to clean. In warehouses with humidity, wash-down areas, or occasional water exposure, that waterproofing is essential.
High hardness. The cured film is hard and durable, resisting indentation from dropped tools, concentrated loads, and the general abuse of industrial operations.
Together, these features create a floor that performs across the full range of warehouse demands—durability, safety, cleanliness, and environmental responsibility.
Marble Effect: Decoration That Belongs in a Warehouse
Here’s where this product genuinely surprises people. It’s not just a functional coating—it’s a marble-effect finish.
The colored sand is distributed through the epoxy film, creating a speckled, stone-like appearance with depth and texture. Combined with the self-leveling smoothness, the result reads as a quartz sand floor with the visual character of natural stone—not a flat, painted surface.
That decorative quality matters more in a warehouse than you might expect. A well-finished floor signals a well-run operation. It improves lighting reflection, brightens the space, and makes the facility look organized and cared for—something that matters during client audits, inspections, and site visits.
And it’s not just about appearance. A high-gloss, seamless surface is easier to clean because dirt and spills sit on top rather than soaking into pores or joints. The floor maintains its appearance with routine maintenance rather than requiring aggressive scrubbing.
Rich, Customizable Colors
The product is available in rich colors, customizable to match a design palette, a brand identity, or a functional color-coding scheme.
In a warehouse, color is a tool. Color-coded zones designate walkways, storage areas, hazardous zones, and equipment footprints. Color can improve visibility, reinforce safety protocols, and support wayfinding in large facilities. And a well-chosen floor color can brighten a space, improve morale, and make the facility look professional.
Because the color comes from mineral aggregate integrated into the coating rather than a surface pigment, it holds up over time rather than fading in traffic lanes. The floor keeps its character through years of use.
Application and Packaging
The product is a two-component system—A resin and B hardener mixed with colored sand—applied by brush for smaller areas and edges, with roller or squeegee options for larger floors. The self-leveling behavior ensures a smooth, even finish with minimal effort.
The shelf life is 12 months, which allows for sensible stock management, and the product is also known as Self-Leveling Epoxy Resin Colored Sand Floor Paint.
Packaging is practical: single item, 11 × 11 × 13.8 cm, 1.12 kg gross weight—a manageable size for sampling, touch-ups, and small projects, with larger configurations available for full-scale warehouse installations.
Where This Floor Belongs
The product is classified for building coating usage and floor surface application, with a feature set that fits naturally into:
- Warehouses and distribution centers – wear-resistant, seamless, and easy to clean
- Industrial workshops – chemical-resistant and durable under machinery
- Storage facilities – dust-free and waterproof
- Logistics hubs – slip-resistant and traffic-ready
- Showrooms and commercial spaces – marble effect with customizable color
- Basements and utility areas – moisture-resistant and easy to maintain
The appliance paint and building coating usage classifications reflect the resin’s broader versatility, but the warehouse floor is where its specifications deliver the most value.
The Technical Snapshot
- Brand: ABTOHE
- Product: Self-Leveling Colored Sand Epoxy Floor Coating
- Other Names: Self-Leveling Epoxy Resin Colored Sand Floor Paint; floor paint
- Place of Origin: Jiangsu, China
- Main Raw Material: Epoxy
- Material: Epoxy resin, curing hardener, colored sand
- State: Liquid coating
- Application: Floor surface
- Usage: Building coating, appliance paint
- Application Method: Brush (roller/squeegee for larger areas)
- CAS No.: 79-10-7 (mixture)
- EINECS No.: 201-177-9
- Molecular Formula: C3H4O2
- Colors: Rich colors, customizable
- Features: Eco-friendly, waterproof, high hardness, wear-resistant
- Shelf Life: 12 months
- Packaging: Single item, 11 × 11 × 13.8 cm, 1.12 kg gross weight
Key advantages:
- Self-leveling for even application without manual leveling
- High wear resistance against scratches and abrasion
- Chemical resistance for demanding industrial environments
- Anti-slip surface for excellent traction and accident prevention
- Customizable colors to match any design or functional requirement
Who This Floor Is For
Warehouse and distribution center operators who need a floor that withstands forklift traffic, chemical spills, and constant use without failing.
Facility managers looking for a seamless, easy-clean surface that reduces maintenance costs and safety incidents.
Contractors who want a self-leveling system that installs efficiently and delivers a consistent, professional finish.
Distributors and buyers seeking a factory-direct product with customizable colors and broad application across industrial and commercial markets.
The Bottom Line
A warehouse floor is the platform everything else runs on. When it performs, nobody notices. When it fails, everything suffers—safety, productivity, cleanliness, and the bottom line.
The ABTOHE Self-Leveling Colored Sand Epoxy Floor Coating is designed for the first scenario. It delivers self-leveling application for even, seamless results, high wear resistance against scratches and abrasion, chemical resistance for demanding industrial environments, an anti-slip surface for safety, eco-friendly, waterproof, high-hardness performance, and a marble-effect, customizable-color finish that makes the floor as attractive as it is durable.
It’s manufactured in Jiangsu, China, backed by a 12-month shelf life, and available in rich, customizable colors.
If your warehouse floor is still bare concrete—dusting, staining, and waiting for its first failure—this is the upgrade that pays for itself quietly, every shift, for years.
ABTOHE Self-Leveling Colored Sand Epoxy Floor Coating. Seamless. Wear-resistant. Safe underfoot. Built for the floor under the work.